Sourcing honey at commercial scale requires more than access to the ingredient. Food manufacturers and brands also need the infrastructure to receive, test, store, process, package, and distribute honey reliably as their needs grow.
At GloryBee, we have continued investing in our facilities, equipment, and technology to bring more of those capabilities together. From our purpose-built honey facility to our high-speed packaging line, these investments help us support commercial customers from bulk ingredient sourcing through finished private label products.
A Facility Built Around Commercial Honey
Our 78,000-square-foot facility in Oregon’s Willamette Valley was designed specifically around the needs of honey production and storage. With the ability to handle 50 million pounds of honey annually and room for growth, the facility gives us the infrastructure to support high-volume and recurring commercial honey needs.
Our broader production and distribution footprint extends across Oregon and Ohio. Proximity to major interstates, rail lines, and ports helps us source ingredients from around the world and efficiently serve customers across the country. Our shipping and logistics capabilities include motor freight, small parcel, air freight, tanker shipments, and customer-arranged pickup.
Investing in High-Speed Packaging
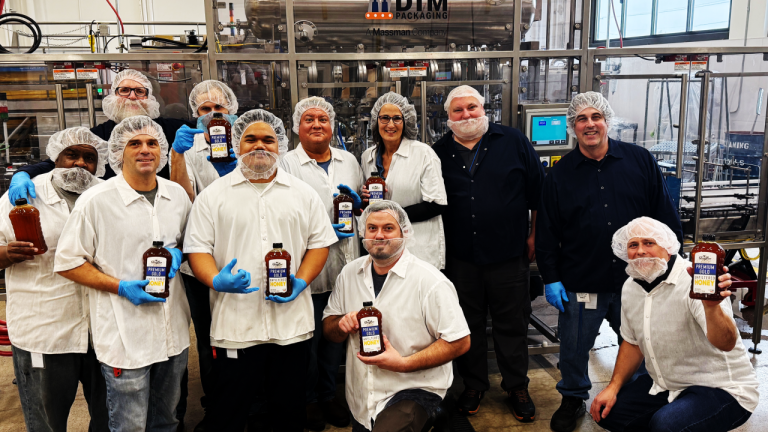
We have also invested in a state-of-the-art manufacturing and packaging line that expands our capabilities for co-packing and premium private label honey.
The automated line combines bottle unscrambling, precision liquid filling, capping, labeling, and inline metal detection. It was designed to increase packaging capacity and flexibility while supporting efficiency, product integrity, and scalability.
Most importantly for our customers, these capabilities allow us to source, fill, label, and ship honey under one roof. Bringing those steps together can help streamline the path from sourcing to a finished product while supporting faster turnaround and greater flexibility as customer needs change.
For brands developing their own honey products, our private label capabilities include glass and plastic packaging in sizes ranging from 12-ounce containers to 5-pound jugs, along with a variety of honey options.
Quality Assurance Throughout the Process
Capacity and speed are only valuable when they’re backed by strong quality systems.
Honey arriving at our facilities is inspected and tested before it is packaged using established food safety standards. Our Quality Assurance team uses multiple testing methods because no single test provides a complete picture of honey quality and authenticity. Our testing requirements include methods addressing purity, adulteration, pollen, antibiotics, microbiological concerns, and other characteristics.
We also work with certifying partners including SQF, True Source, Organic, Non-GMO Project Verified, and OU Kosher. These systems help us support commercial customers with different product, sourcing, and certification requirements.
Supporting Customers Beyond Production
Our capabilities extend beyond receiving and packaging honey.
Our Research, Development and Innovation team brings technical expertise to product development and ingredient applications. We can work with customers on formulation, ingredient functionality, product concepts, sensory considerations, and other technical challenges that arise when bringing a product to market.
That support is backed by a sourcing network with connections in more than 30 countries. Different honey varieties can bring distinct flavor, color, and functional characteristics, and our team can help customers evaluate options based on their application and brand objectives.
Built to Support Commercial Honey Customers
For food manufacturers, private label brands, and other commercial honey buyers, facilities and equipment ultimately matter because of what they make possible: dependable supply, consistent quality, flexible packaging, efficient fulfillment, and room to scale.
At GloryBee, we continue to invest in the infrastructure, technology, and expertise needed to support customers throughout the process. Whether you need bulk honey, private label packaging, or technical support for a new product, contact a honey expert today to discuss how our sourcing, production, packaging, and fulfillment capabilities can support your operation.